


 영어
 스페인어

MXB-JTWN 나사 구멍이 없는 미터식 스러스트 와셔
Cat:자기 윤활 베어링
MXB-JTW 미터법 스러스트 와셔는 고강도 황동(ZCuZn25Al6)을 기반으로 하며 고체 윤활제(흑연 또는 이황화 몰리브덴)가 윤활 매체로 매트릭스에 내장되어 기존 주석 청동을 대체합니다. 이 제품은 안정적이고 효율적인 하중 분배를 제공하고 차량 변속기 및 기...
자세히보다Technical Background and Industry Pain Points
In the precision machining of thin-walled tubes (such as aerospace hydraulic tubes and semiconductor reaction chambers), traditional single-end clamping systems suffer from two core issues:
l Insufficient chatter suppression: The free end experiences forced vibrations with amplitudes of 5-20μm under cutting force excitation (data source: CIRP Annals 2021, 70(1), 357-360), resulting in surface roughness Ra values deteriorating to above 3.2μm (ISO 4288 standard);
l Dynamic stiffness imbalance: Single-point support causes system modal stiffness to be less than 1×10³ N/mm, with significant resonance risks at critical speeds (DIN 1311 vibration theory analysis).
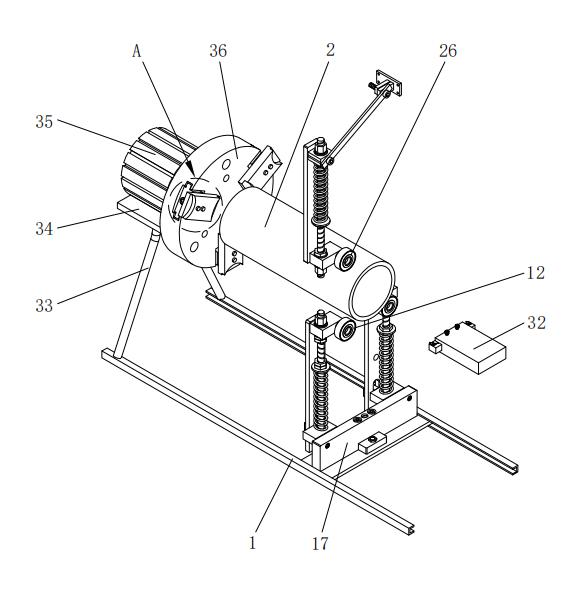
Core Technology Innovation Analysis
I. Multi-Degree-of-Freedom Vibration Suppression System
1.1 Three-Point Constraint Topology Structure
Bottom Dual Support Wheels (12):
l Utilize high-carbon chromium steel (GCr15) wheel bodies with curvature radii R matching the workpiece outer diameter (tolerance ±0.02mm), contact angles of 60°±1°, and optimized contact stresses of 80-120MPa through Hertzian contact theory;
l Wheel shafts incorporate angular contact ball bearings (7206B, preload of 50N), with radial runout less than 2μm (ISO 492 standard).
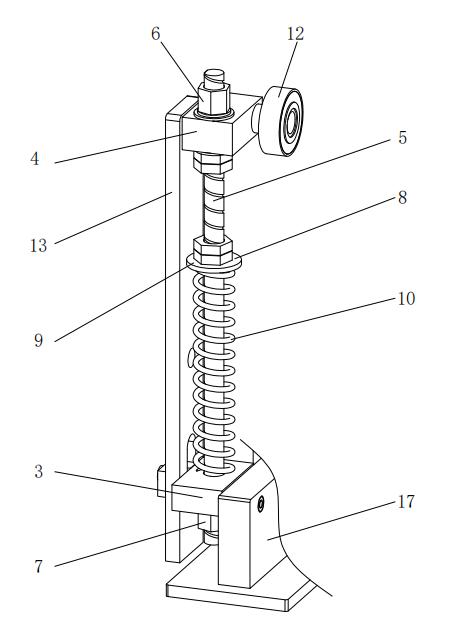
Top Adjustable Pressure Wheel (26):
l Apply dynamic preload force F=200±10N via a pressure spring (31) for closed-loop force control;
l Pressure wheel surface laser-clad with WC-10Co coating, with a friction coefficient μ≤0.08 (ASTM G99 testing).
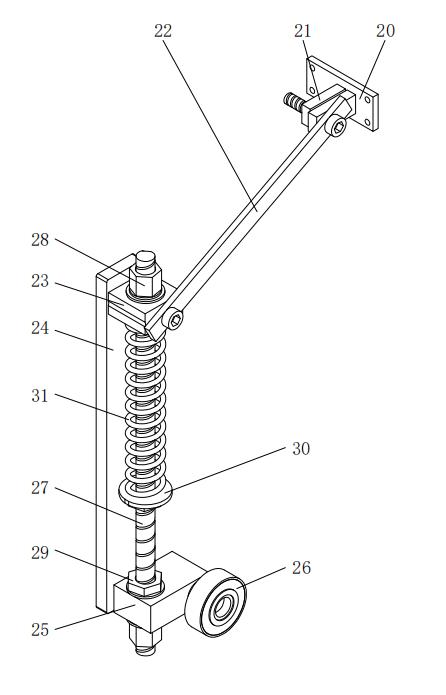
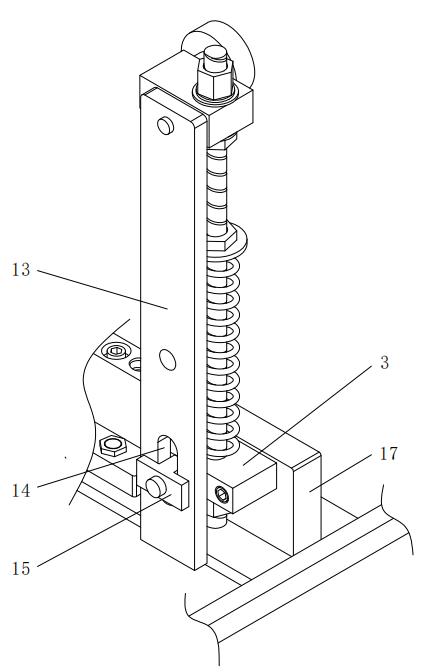
1.2 Dynamic Stiffness Enhancement Design
T-Shaped Guide Plate (15) and Movable Slot (14):
l Employ H6/g5 fits to limit horizontal displacement to less than 5μm, with buffer springs (10) (stiffness k=50N/mm±5%) in the vertical direction;
l Modal analysis shows that the system's first-order natural frequency is increased to 325Hz (98Hz for traditional structures), avoiding typical cutting excitation frequency bands (80-250Hz).
II. Adaptive Force Control System
2.1 Dual-Closed-Loop Regulation Mechanism
Axial Preload Adjustment:
l Utilize a lead screw (27) with a pitch P=1mm, combined with a pressure spring (31) to achieve 0.05-0.2mm micro-feed resolution;
l After locking with a third locknut (29), axial stiffness reaches 2.5×10⁴ N/mm (ISO 10791-2 testing).
Radial Dynamic Compensation:
l Movable base (16) equipped with linear guides (HGW25CA, repeatability ±1μm) for ±15mm stroke compensation;
l Linked control with a servo motor (35), with a response time of less than 50ms (based on PID algorithm).
2.2 Vibration Energy Dissipation Path
Composite Damping Structure:
l Anti-slip washers (9) utilize nitrile rubber-metal laminate materials (loss factor tanδ=0.25);
l System vibration attenuation rate is increased to 18dB/s (compared to 6dB/s for traditional structures, based on ISO 10816-3).
Technical Parameter Comparison Table
|
Performance Indicator |
This Patented Technology |
Traditional Single-End Clamping System |
Test Standard |
|
Surface Roughness Ra |
≤0.8μm |
≥3.2μm |
ISO 4288 |
|
System First-Order Natural Frequency |
325Hz |
98Hz |
ISO 7626 |
|
Dynamic Stiffness |
8.2×10³ N/mm |
1.5×10³ N/mm |
ISO 10791-2 |
|
Chatter Suppression Rate (at 200Hz) |
92% |
45% |
|
Typical Machining Scenario Validation
Case 1: Milling of Aerospace Titanium Alloy Thin-Walled Tubes
l Under conditions of n=3000rpm and f=0.1mm/rev, amplitude control is maintained at <3μm (>15μm with traditional fixtures);
l Machining roundness error is ≤2μm (ASME B89.3.4 standard requires ≤5μm).
Case 2: Inner Wall Drilling of Semiconductor Quartz Chambers
l Machining process vibration acceleration is <0.5g (>2.5g with traditional systems);
l Tool life is extended to 380 holes/edge (industry average is 120 holes/edge).
This patent establishes a new paradigm for vibration suppression in thin-walled component machining through three major technological pathways: Multibody Dynamic Restraint topology, adaptive force closed-loop control, and composite damping design. Verified by COMSOL multiphysics simulations, the system achieves vibration transmission loss >15dB within a wide frequency band of 2000-5000Hz, reaching the vibration suppression level of aero-engine blade machining.
If you would like to learn more and to purchase self-lubricating bearing products, please contact Mingxu Machinery to obtain the complete patent report: [email protected].
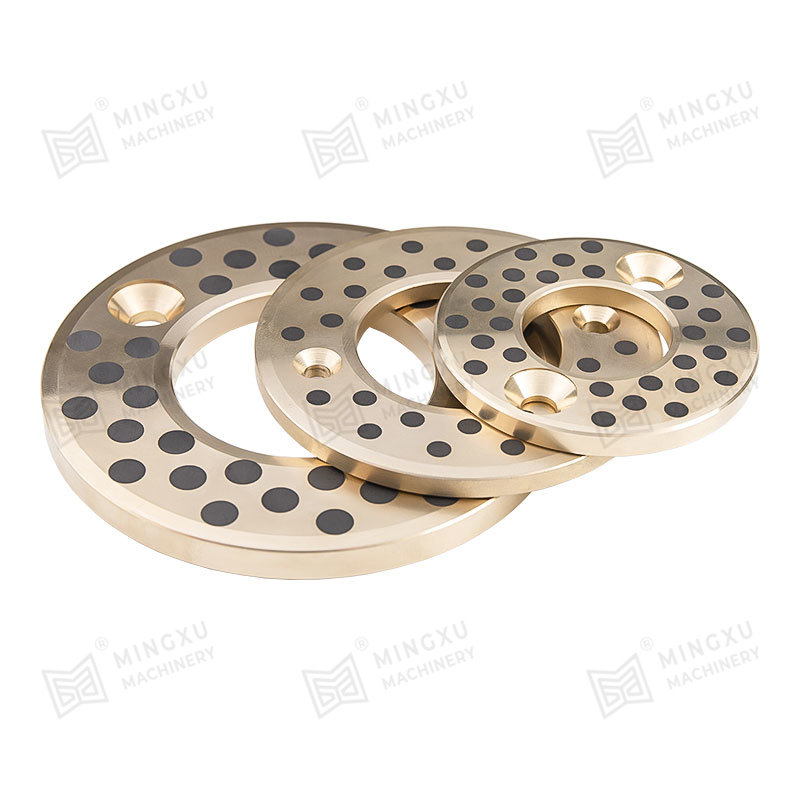
MXB-JTW 미터법 스러스트 와셔는 고강도 황동(ZCuZn25Al6)을 기반으로 하며 고체 윤활제(흑연 또는 이황화 몰리브덴)가 윤활 매체로 매트릭스에 내장되어 기존 주석 청동을 대체합니다. 이 제품은 안정적이고 효율적인 하중 분배를 제공하고 차량 변속기 및 기...
자세히보다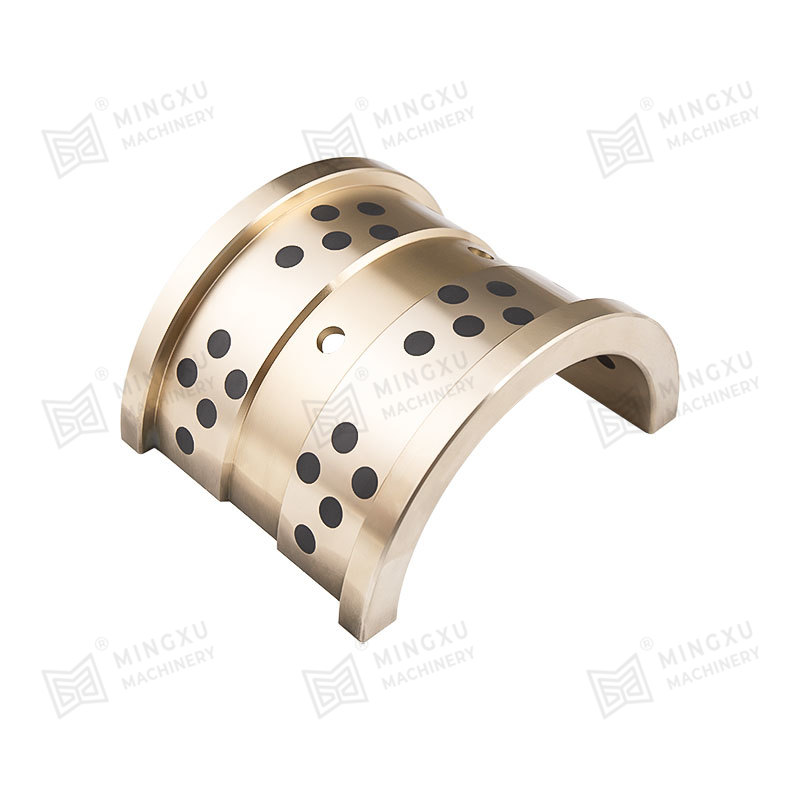
MXB-JFFB 자체 윤활 하프 베어링은 샤프트 또는 액슬 원주의 절반만 덮고 회전 기계에 대한 지지력을 제공하고 마찰을 줄이는 베어링을 의미합니다. 하프 베어링은 회전 부품의 원활하고 효율적인 작동에 중요한 역할을 하며 자동차 엔진, 산업 기계 및 기타 기계 시...
자세히보다
MXB-JDBS 청동 기반 솔리드 상감 자체 윤활 구형 베어링은 구형 슬라이딩 베어링입니다. 슬라이딩 접촉면은 내부 구면과 외부 구면입니다. 이동 중에 어떤 각도로든 회전하고 흔들릴 수 있습니다. 표면 인산염 처리, 튀김 입, 패딩, 스프레이 등 다양한 특수 공정...
자세히보다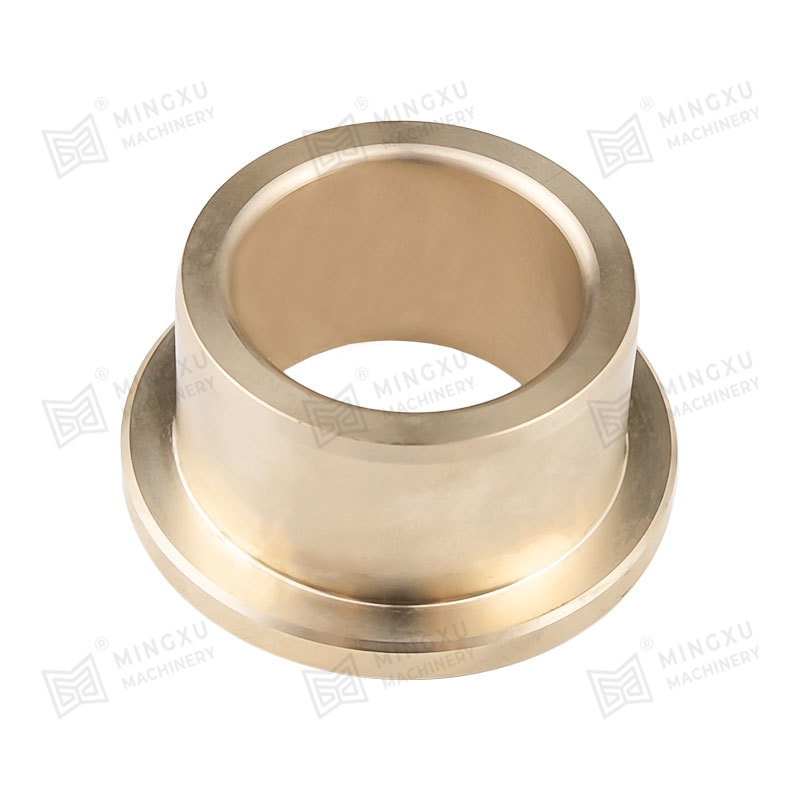
MXB-JDBUF 자기 윤활 주조 청동 베어링은 자기 윤활 및 플랜지 설계의 장점을 결합합니다. 원료는 내구성, 내마모성 및 내식성을 보장하기 위해 고품질 주조 청동 재료로 만들어졌습니다. 내장된 고체 윤활제(흑연 등)는 자체 윤활 특성을 갖고 있어 추가 윤활이 ...
자세히보다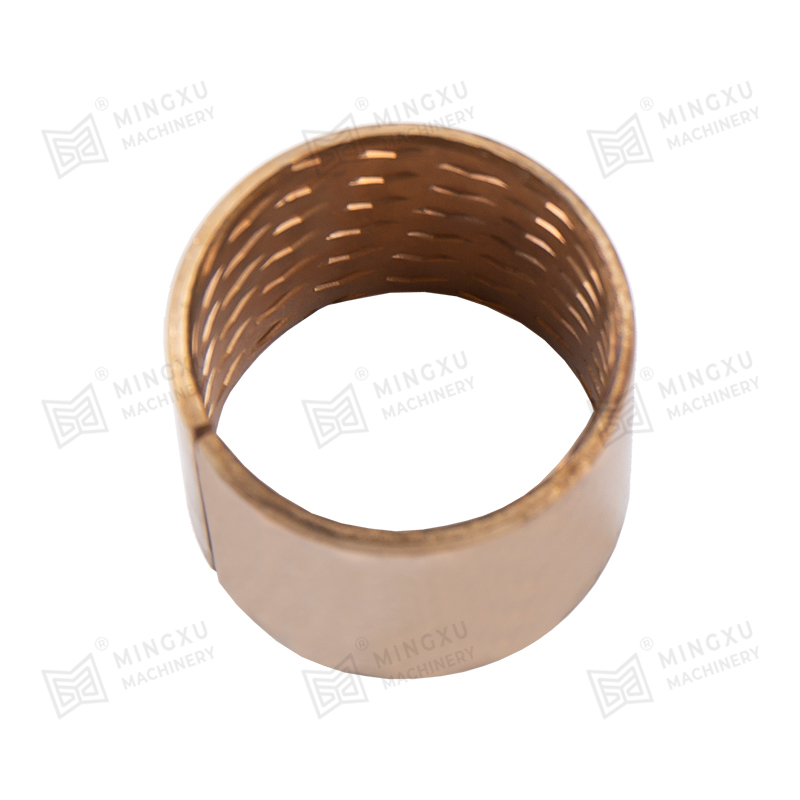
MXB-FB090 청동 코일 베어링은 CuSn8 청동으로 압연되어 높은 부하 용량과 우수한 내마모성을 갖춘 경제적인 베어링입니다. FB090 제품의 작업 표면은 일반적인 다이아몬드 모양의 오일 구멍으로 덮여 있습니다. FB092 제품의 작업 표면은 오일 저장 역할...
자세히보다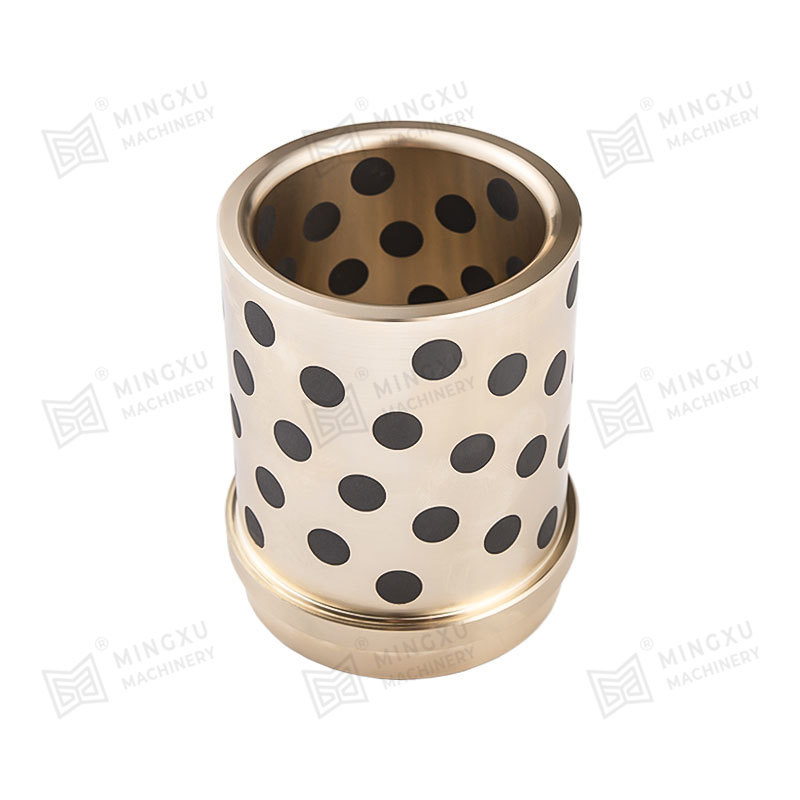
MGB61 NAAMS 표준 가이드 부싱은 정확하고 부드러운 가이드 적용을 위한 신뢰할 수 있는 솔루션입니다. 이 가이드 부싱은 NAAMS 표준을 충족하도록 설계되어 다양한 시스템에 대한 적합성을 보장합니다. 1. 금형 제조 산업에 적합하며 널리 사용됩니다. ...
자세히보다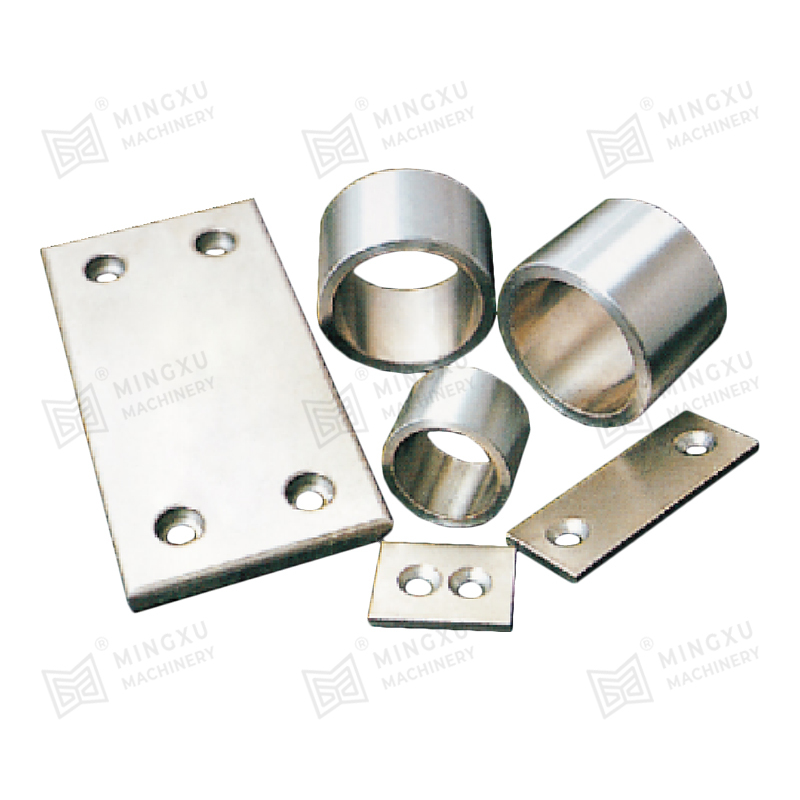
MX2000-2 니켈 흑연 분산 합금 베어링은 고체 윤활 베어링 중 신제품입니다. TF-1과 비교하여 이 제품은 녹 방지 및 고온 저항이 우수한 특성을 가지고 있습니다. 야외에서 사용되는 철도 스위치 슬라이더에 매우 적합합니다. 내마모성이 뛰어나고 유지 관리가 필...
자세히보다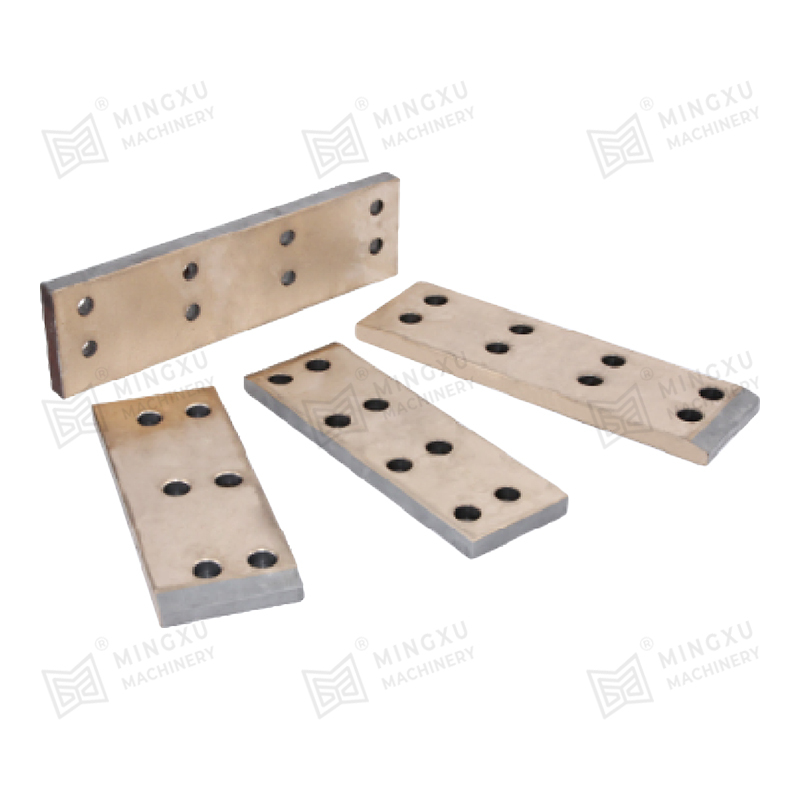
3면에 내마모성 합금이 소결된 바이메탈 슬라이드 플레이트는 새로운 유형의 자기 윤활 플레이트입니다. 일반적인 단면 또는 양면 소결 바이메탈 슬라이드 판과 비교하여 제품의 소결 합금층 표면이 3면이므로 더 많은 윤활을 제공할 수 있습니다. 동합금 슬라이드판에 비해 ...
자세히보다
SF-1W 무연 베어링은 국제 환경 보호 요구 사항에 따라 SF-1X 소재를 기반으로 개발된 신제품입니다. 이 제품은 일반 기계에 널리 사용되는 것 외에도 특히 식품 기계, 제약 기계, 담배 기계에 적합합니다. 무연 효과는 유럽 건강 표준을 충족하며 오일 프리 윤...
자세히보다
SF-PK PEEK 삼중 복합 베어링은 강판, 구리 분말층, PTFE 충전재로 구성된 새로운 슬라이딩 베어링입니다. 주요 성능은 폴리머, 내열성, 내마모성 및 내식성 소재인 표면 PEEK 소재에 반영됩니다. 특히 물 윤활 및 저유 윤활의 경우 성능이 더욱 우수합니...
자세히보다



문의하기